Scantek 2000 CNC Lathe – First cut with LinuxCNC

I converted my Scantek 2000 CNC lathe to work via Parallel port control (for Mach3/LinuxCNC software control) and have been learning how to hand write gcode (because the Linux compatible CAM lathe software options are not terribly good).
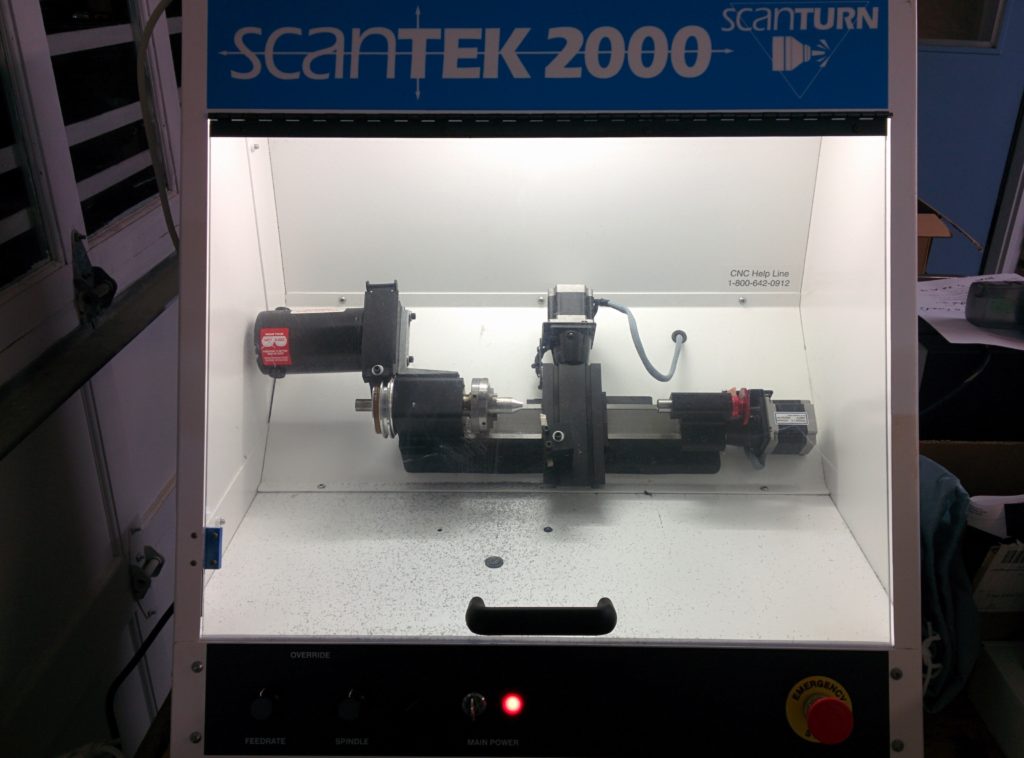
IMG_20160415_220855

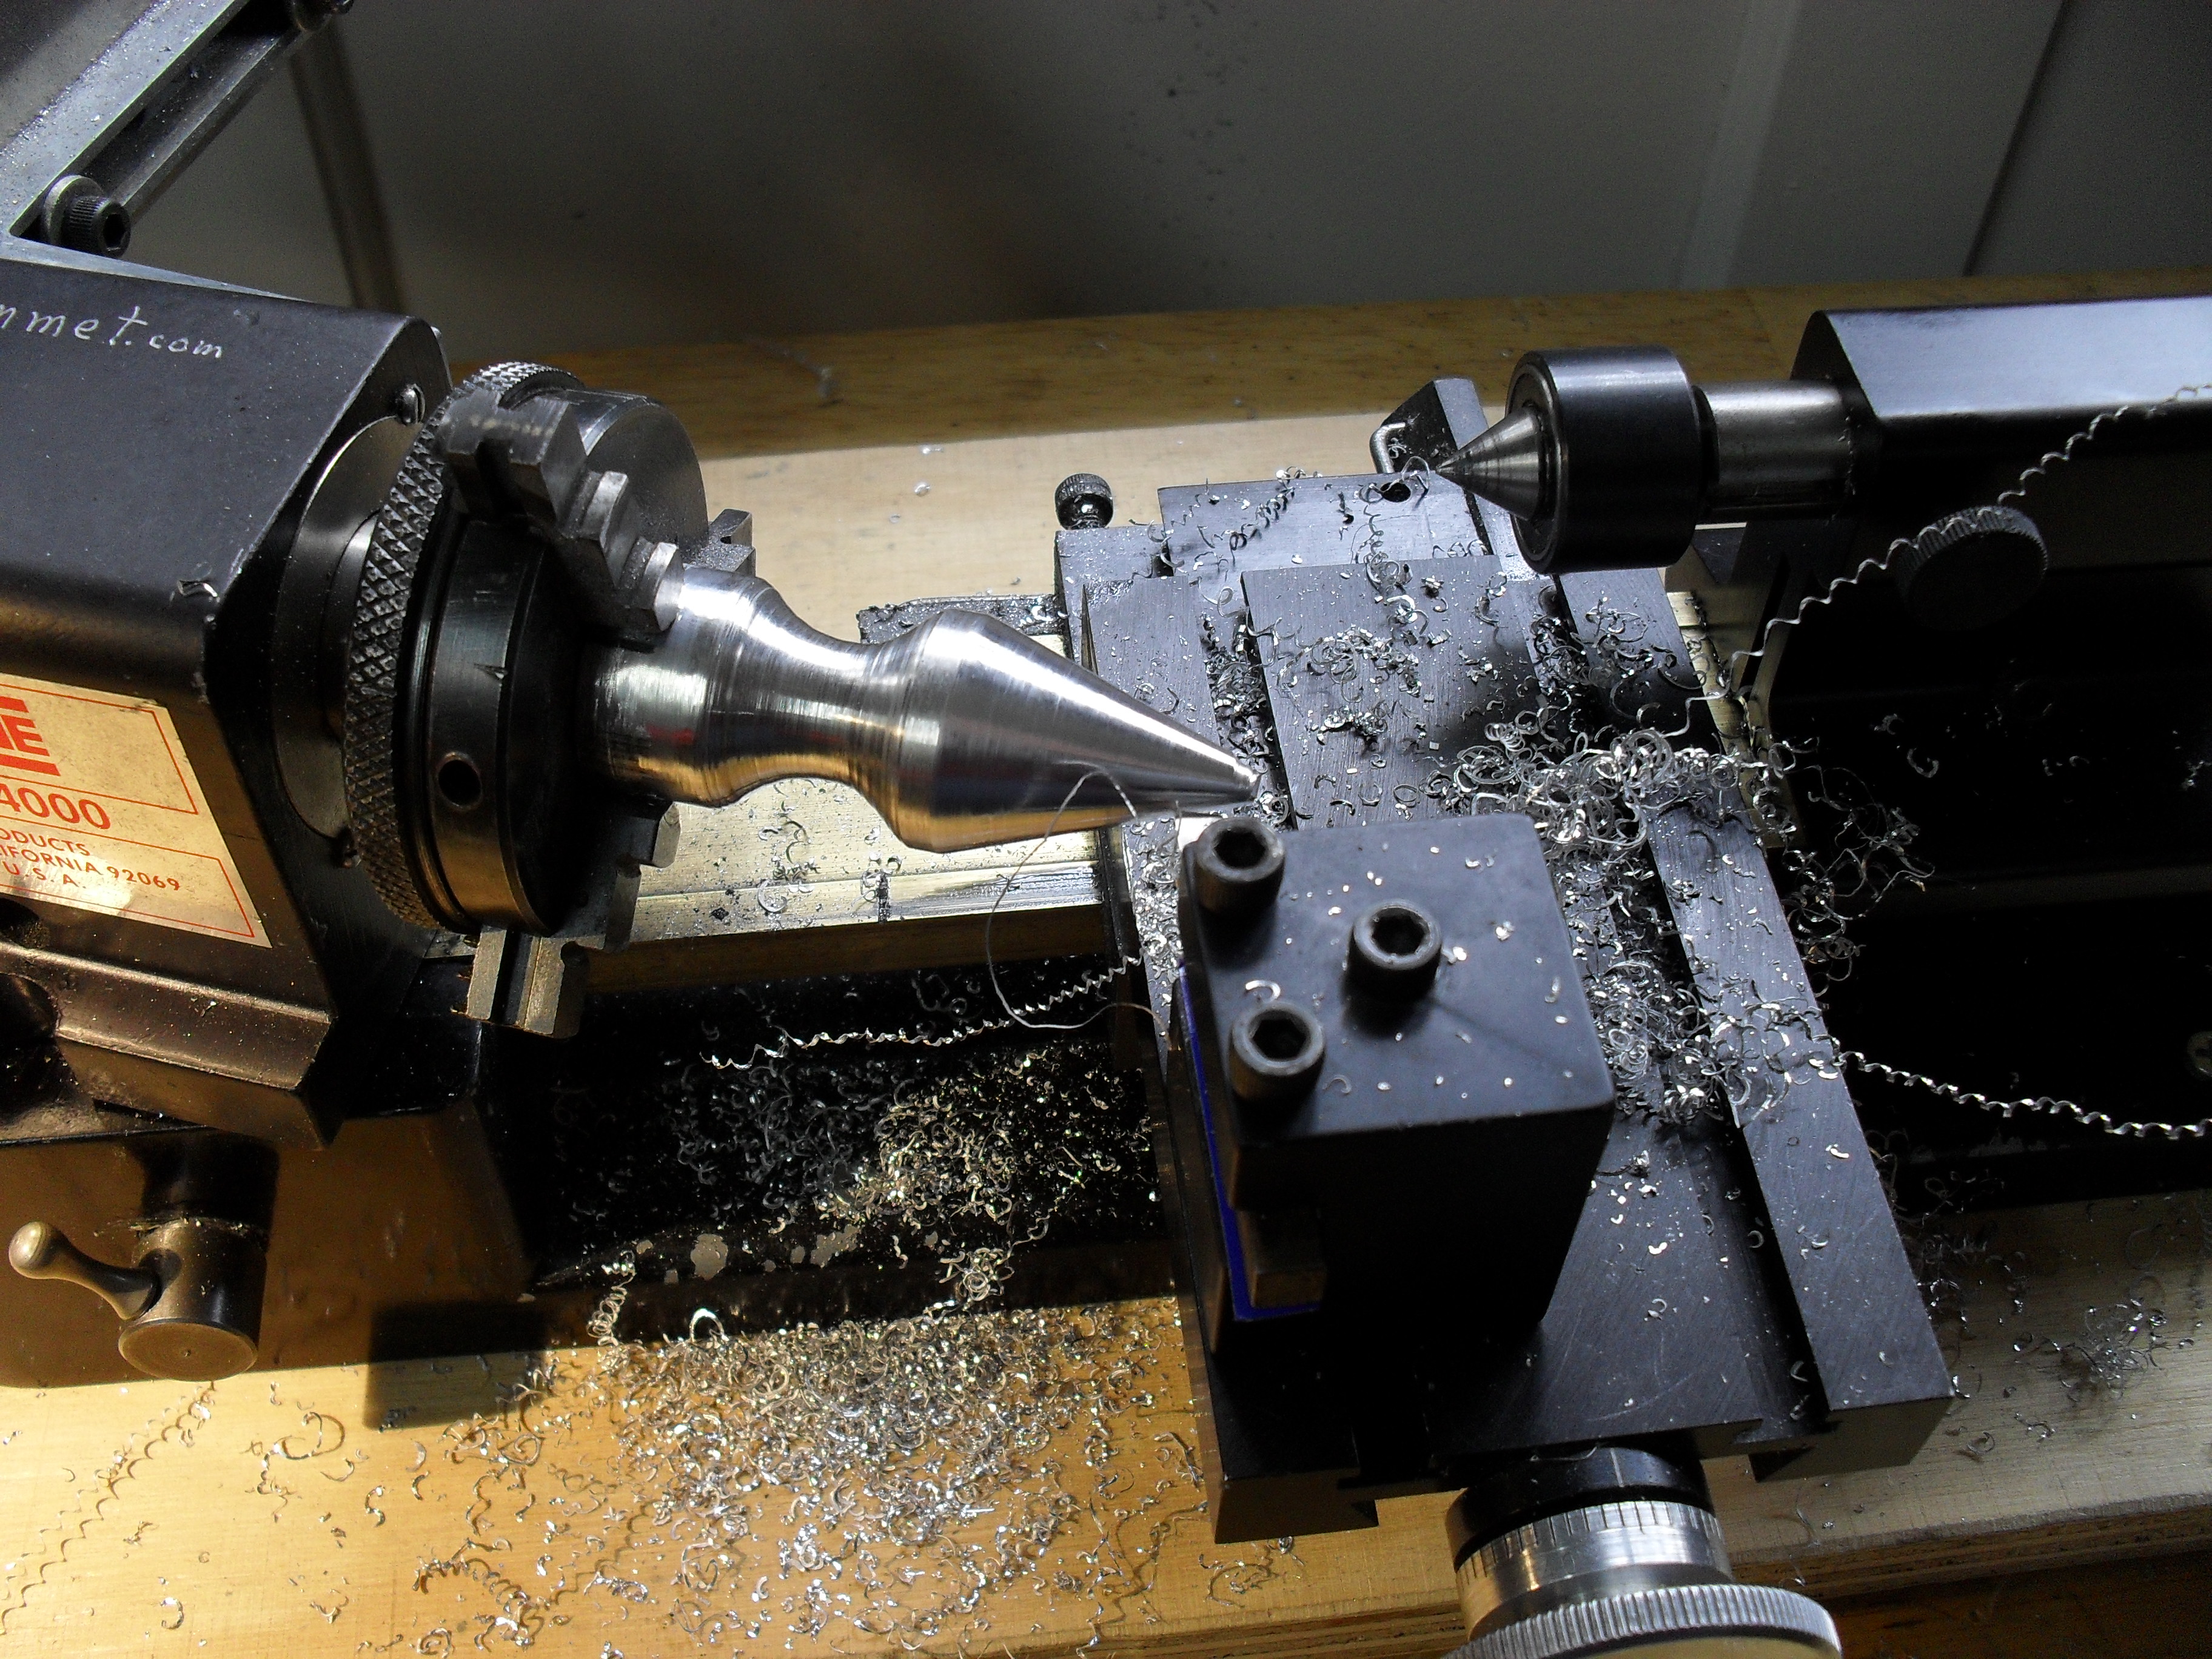
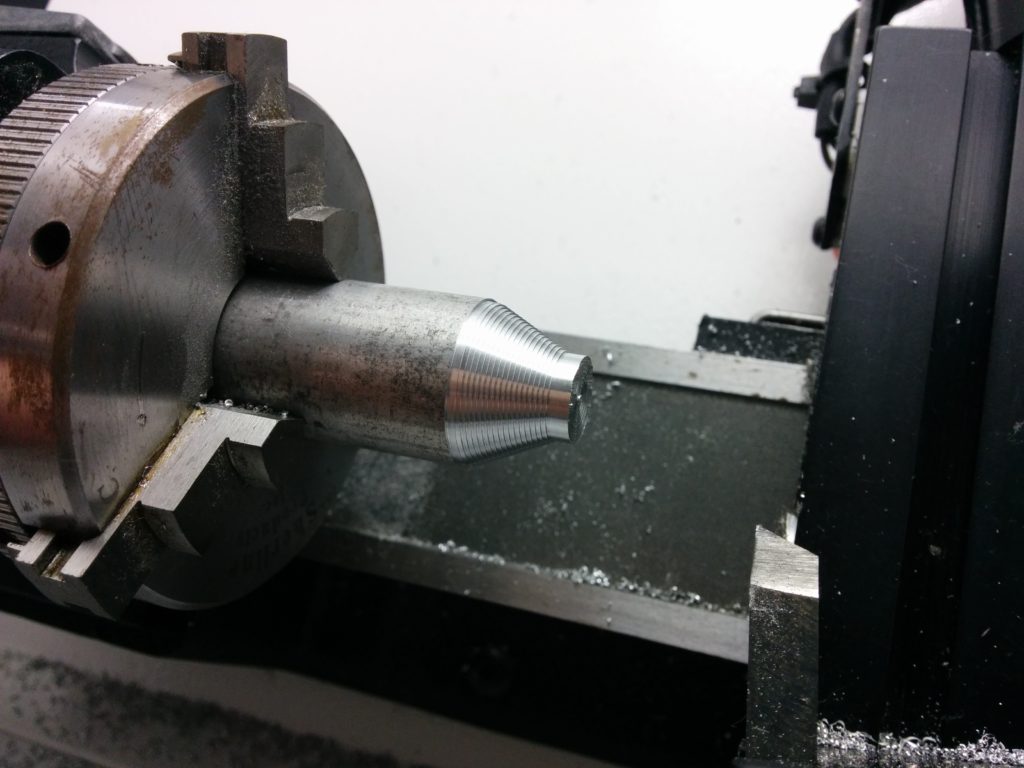
Unfortunately, the LinuxCNC   software doesn’t support many of the automated cycles (G71 I’m looking at you!) for lathe turning (yet!), so I had to write up a gcode file with many manual G1 passes to cut down the cone shape you see here.
IMG_20160415_220832

Instead of hand coding the whole thing, I wrote a small python script that automated the gcode generation, which takes 0.2 mm passes off the stock, stopping 0.5mm shorter each time from 10mm down to 5mm radius. But I did the first few by hand….

Here is a video of the process in action:

And below is the full gcode file for those who care….

Continue reading →
oneTesla top breakout point for my musical Tesla coil

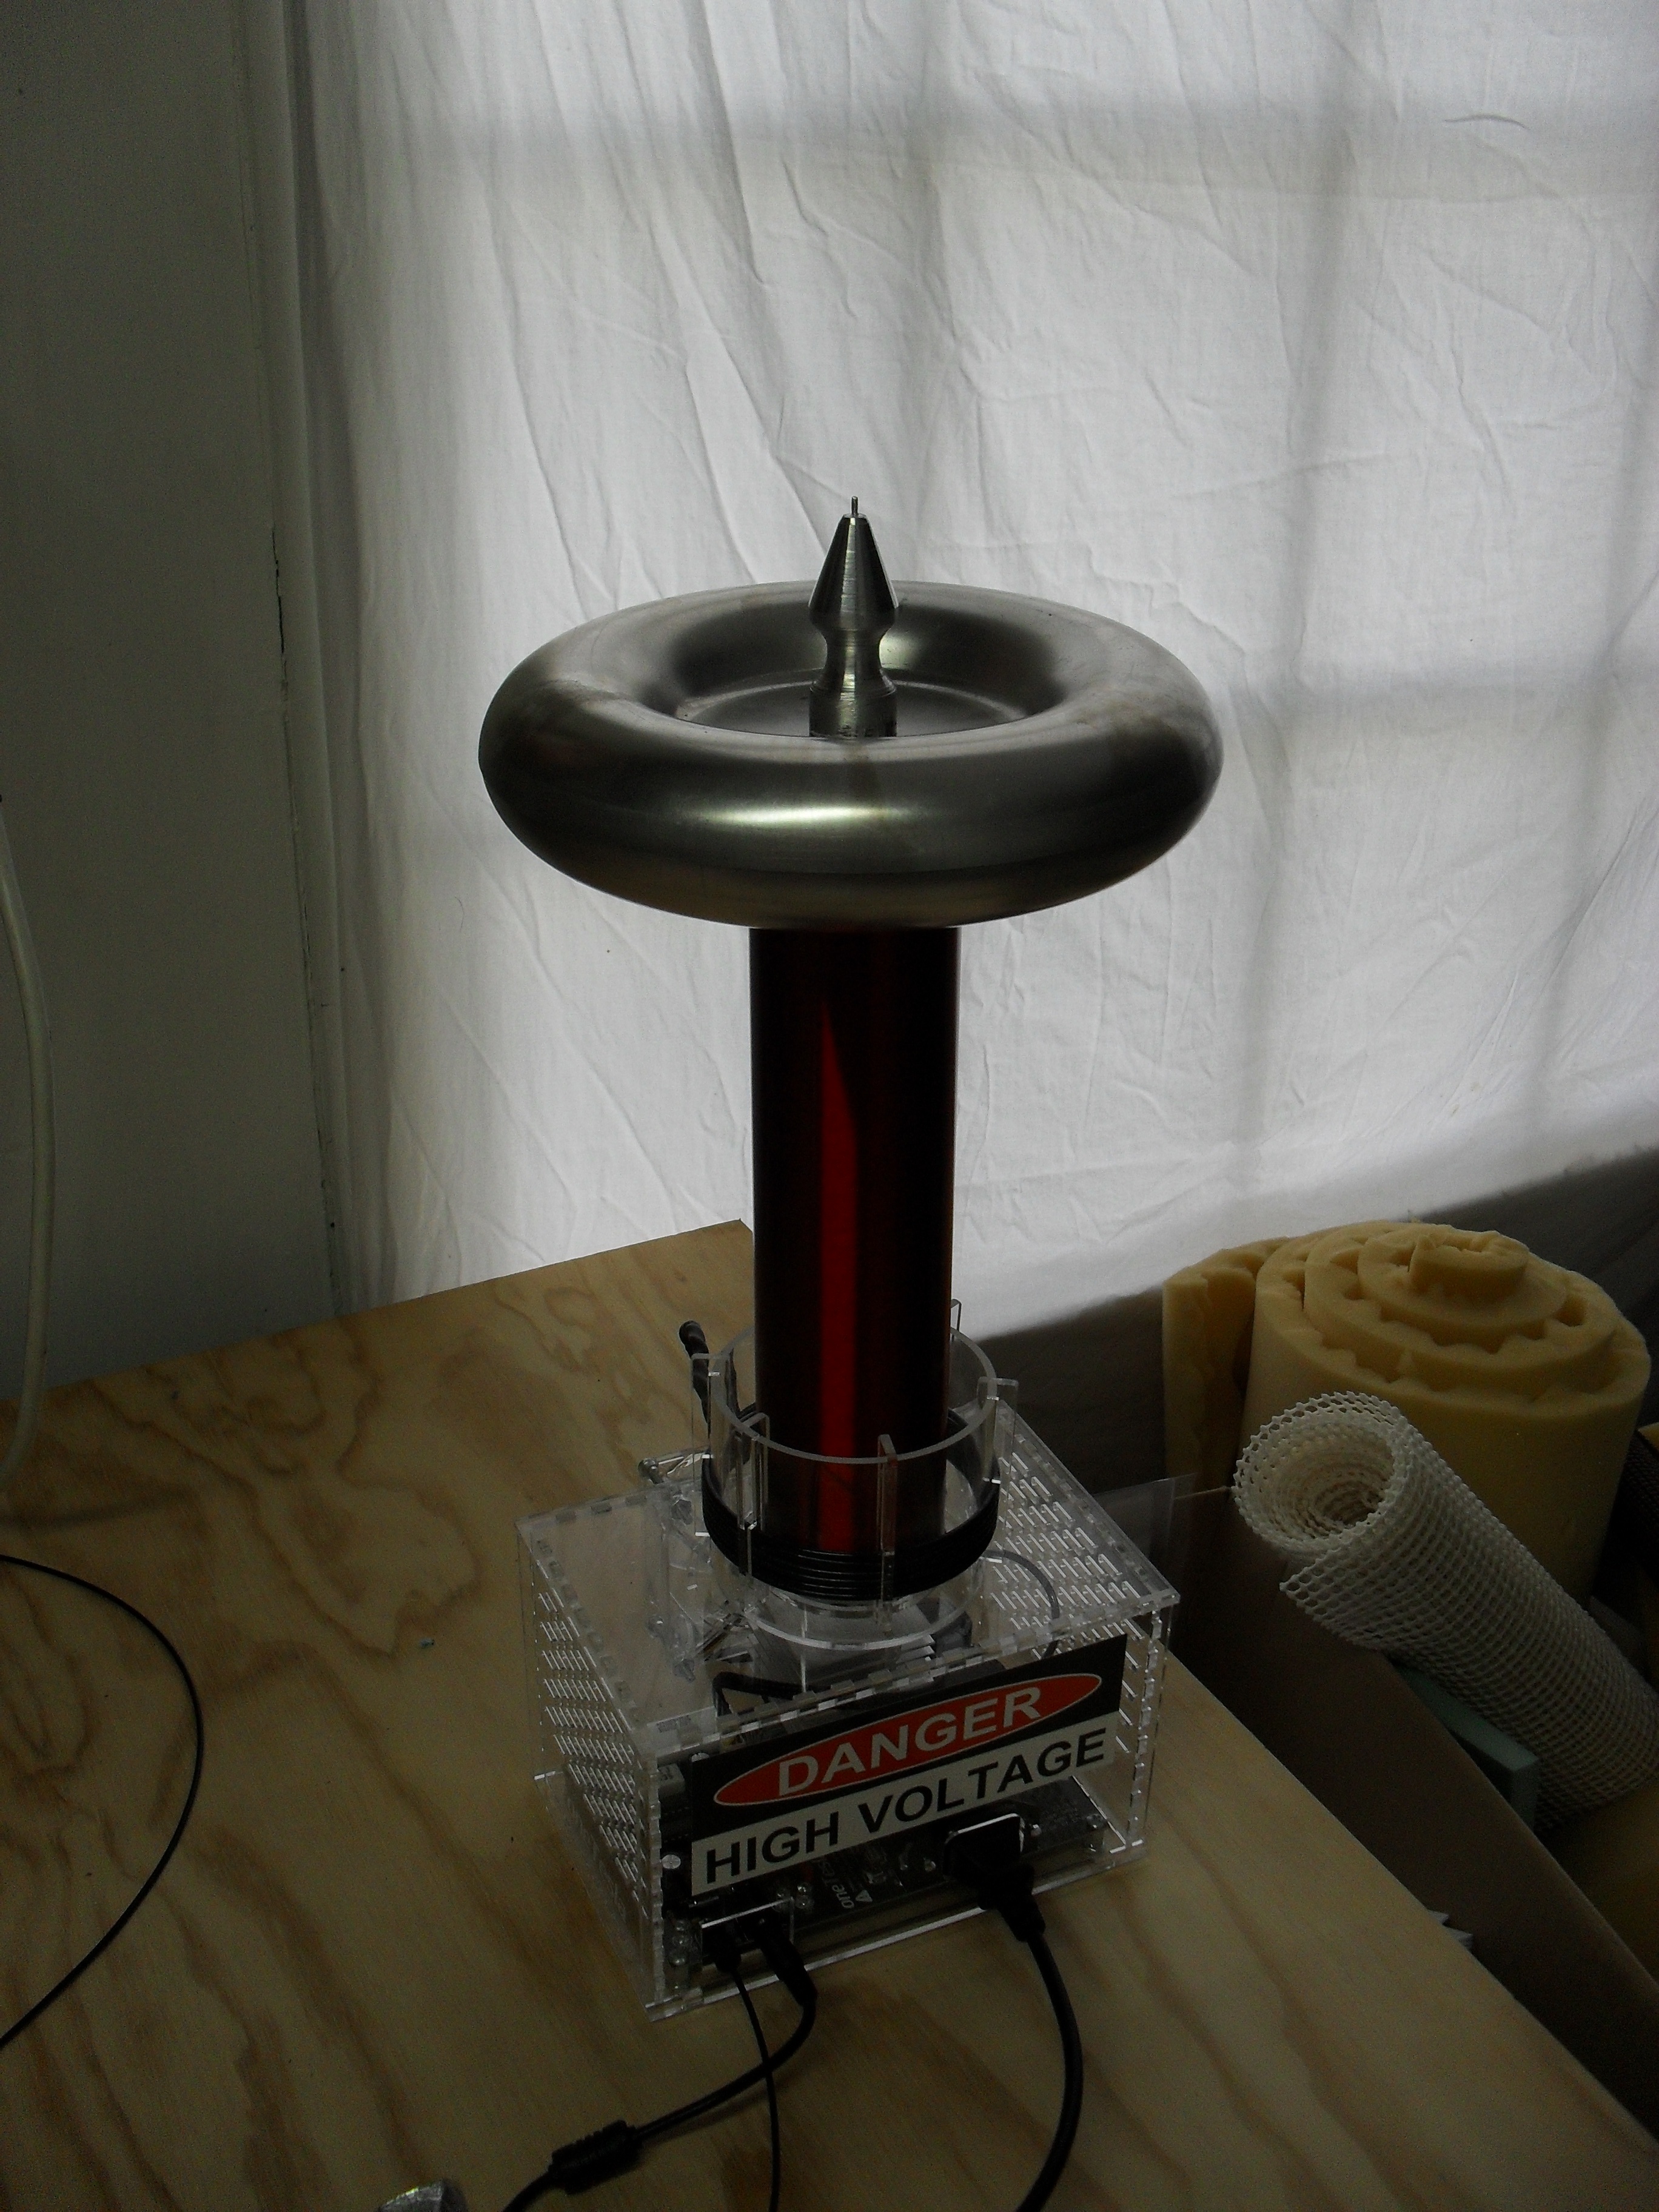
Since I’ll be primarily using my oneTesla to play music, I wanted a top facing breakout (so the sparks will shoot up, instead of out to the side). Also, I wanted something more professional looking than a stick of metal taped to the top of the toroid. Here is the final product on the top of my toroid:

You can visit [ this post ] to see a video of it in action.
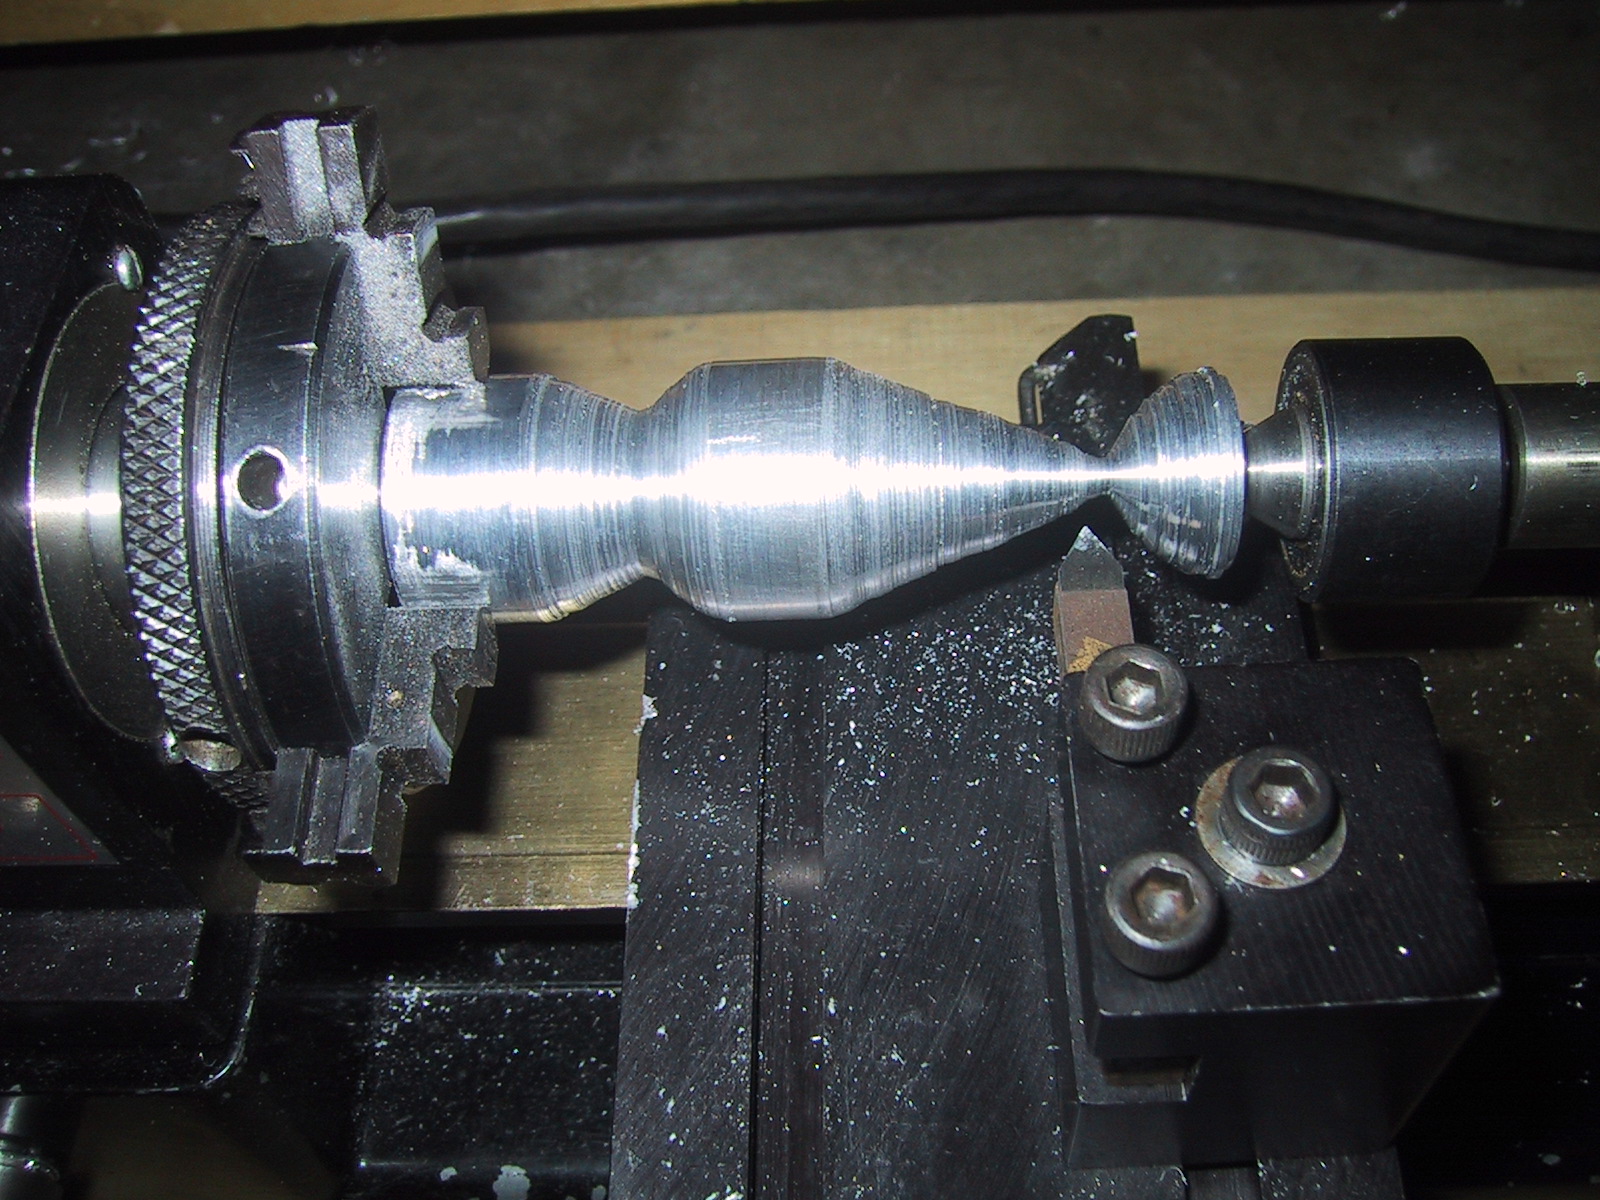
I used the lathe to get the general shape I wanted:
on_lathe

Then turned it to even up the 15 degree angle:

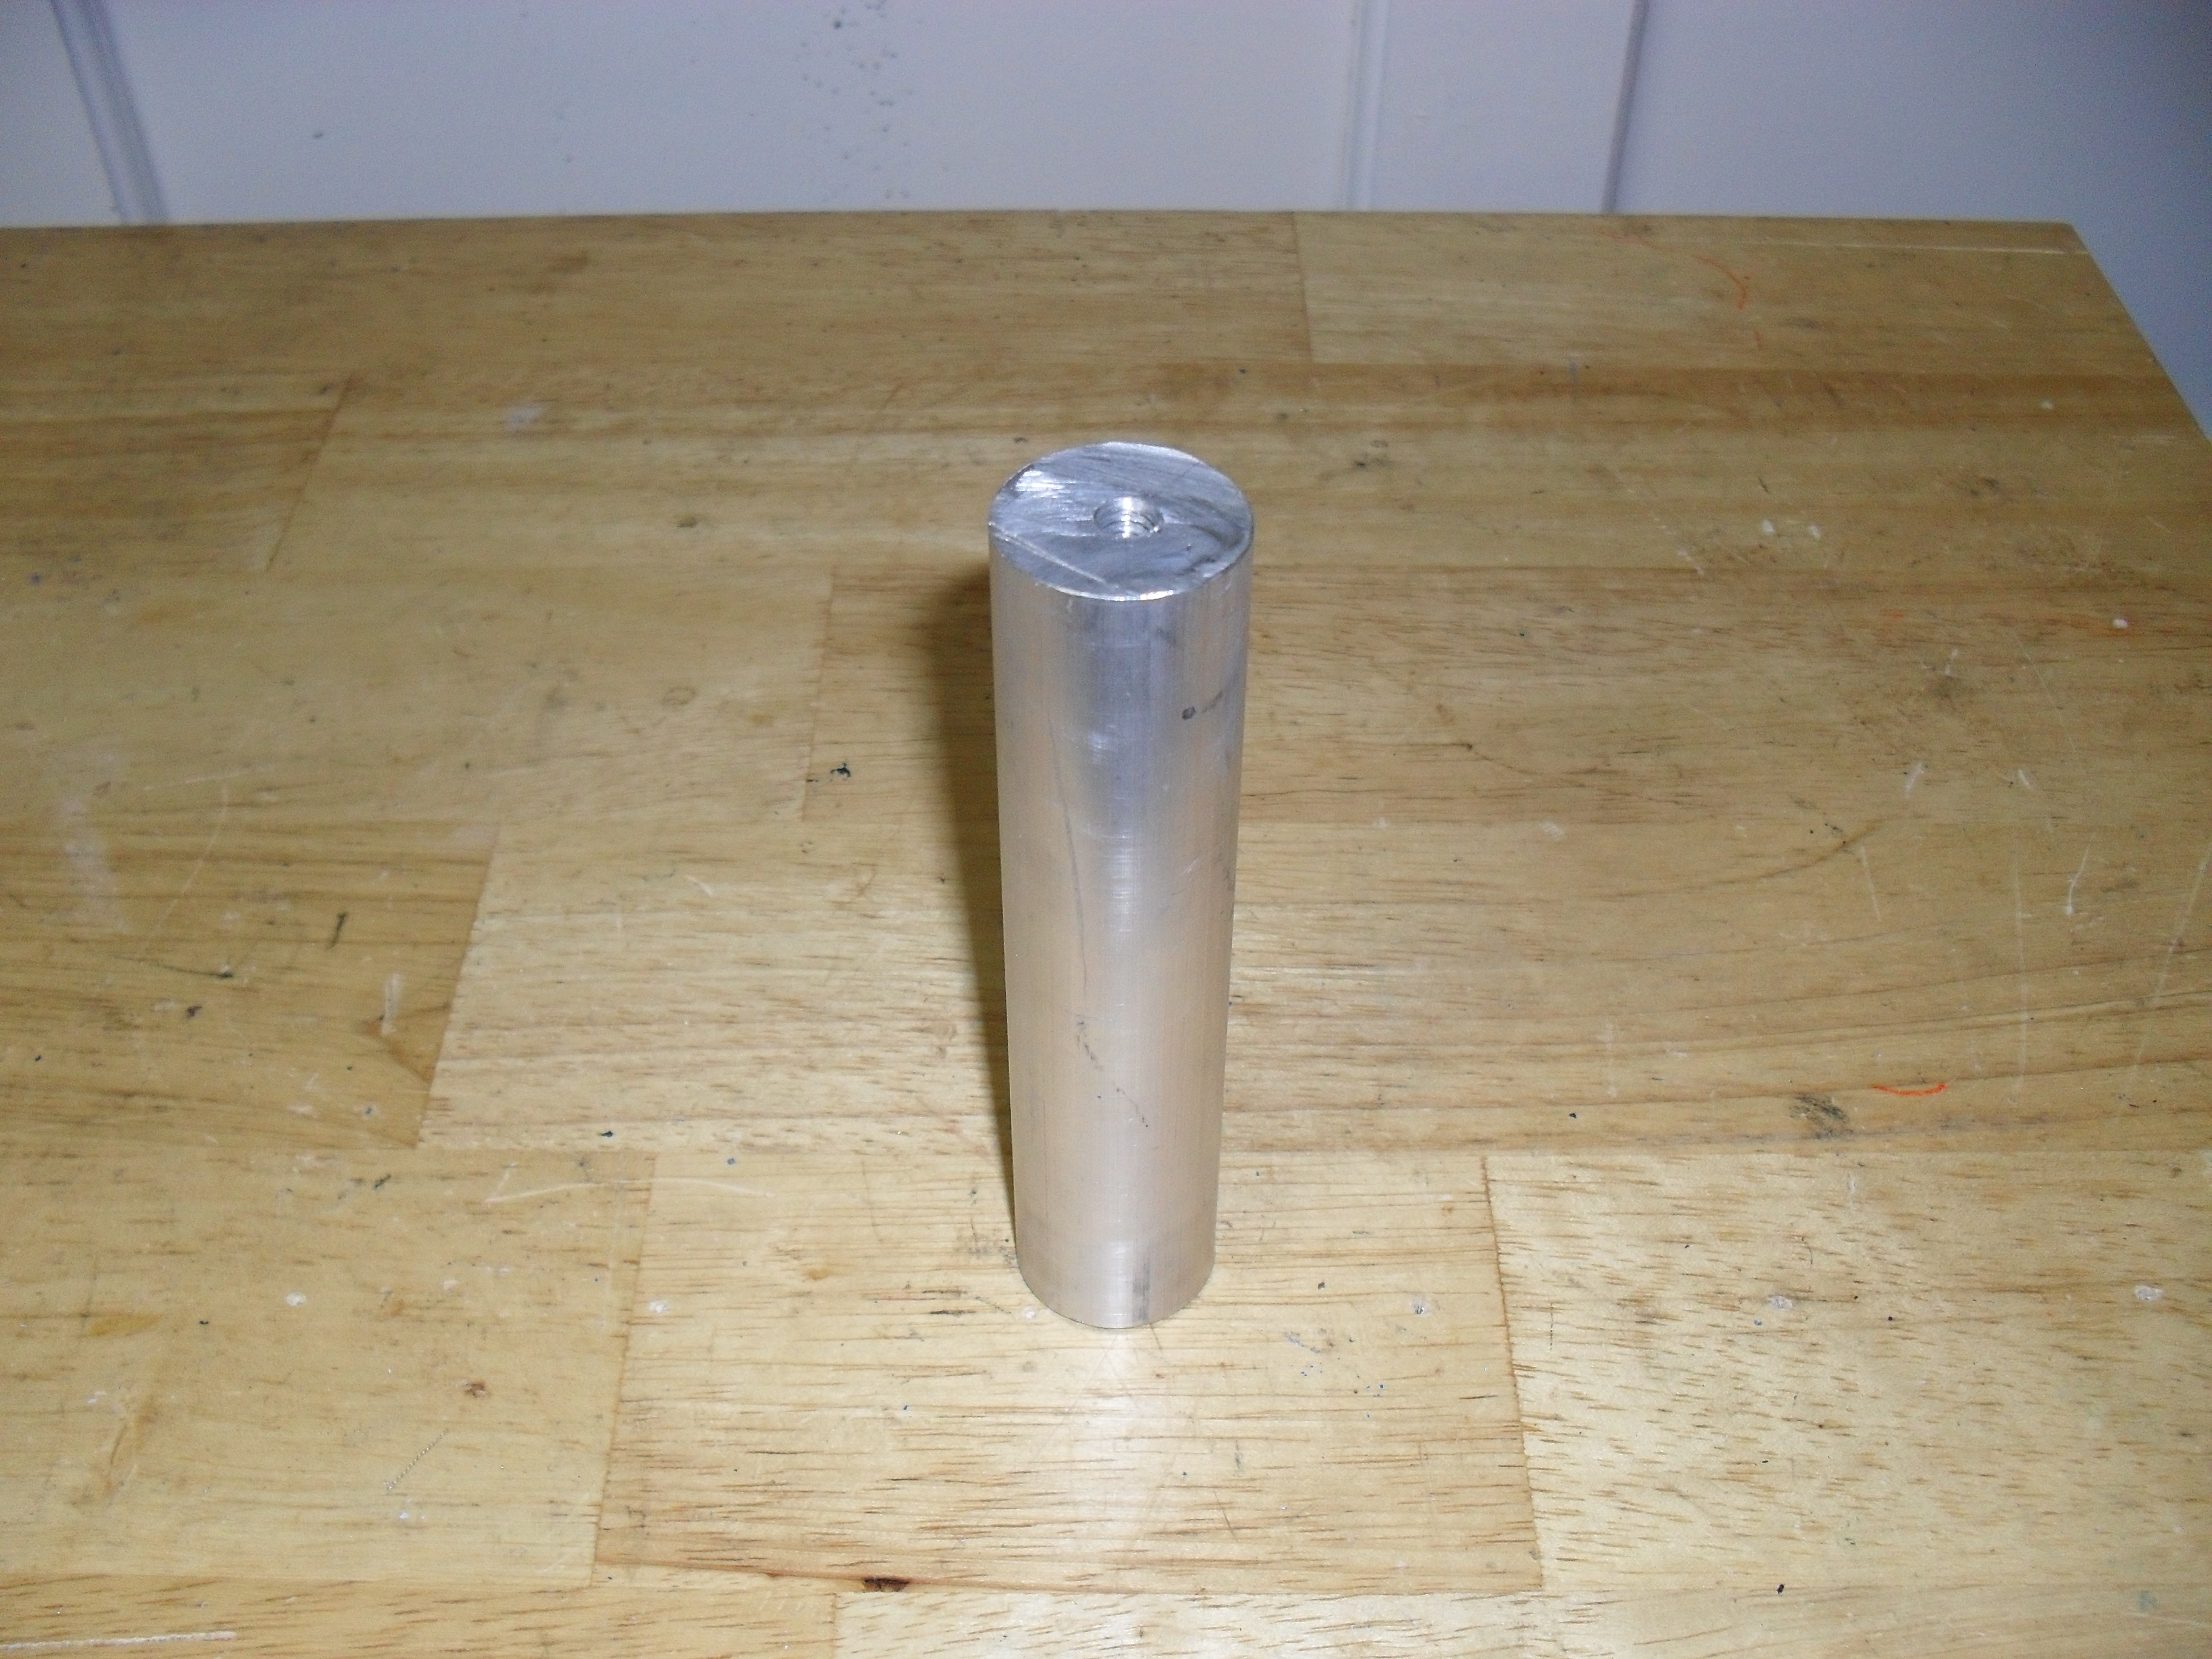
And this is my original 1″ diameter aluminum stock. I tapped it for the 14-20 bolt on the top of my Tesla coil that normally has a wing nut to hold the stamped toroid together, so the whole thing just screws onto the top.

Turning custom extruder parts

finished_heatsinc
jays_parts_in_front

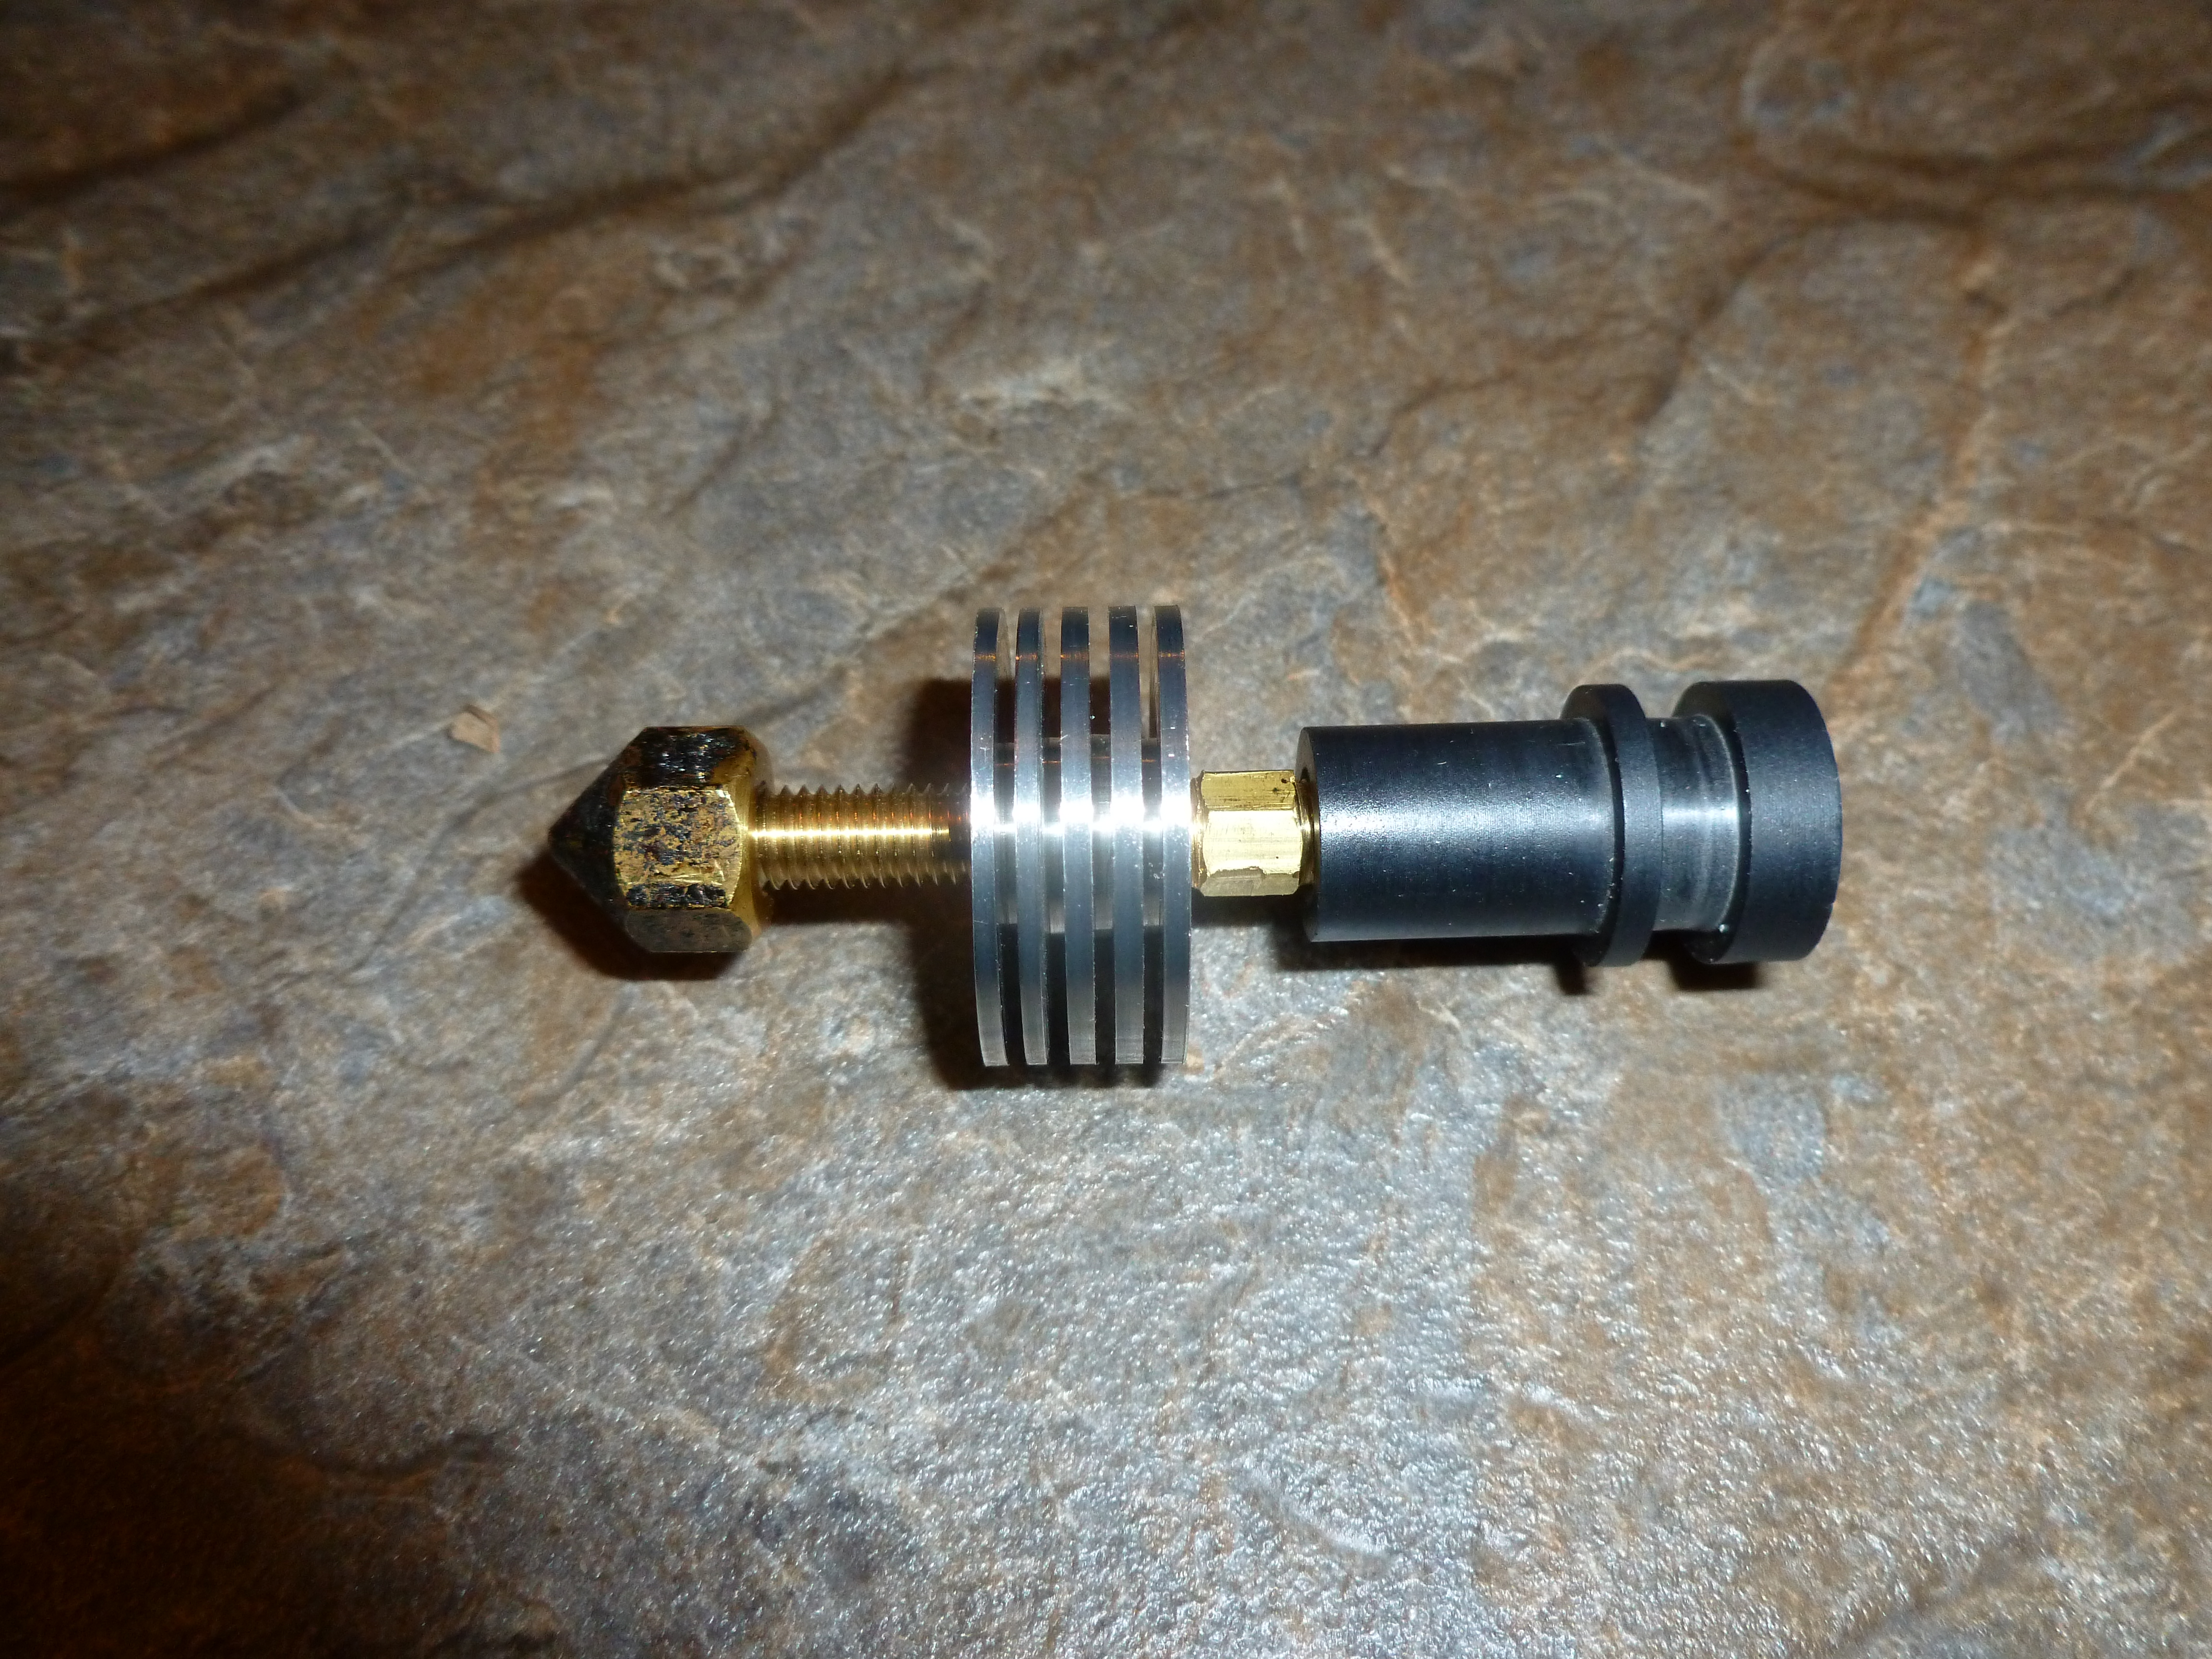
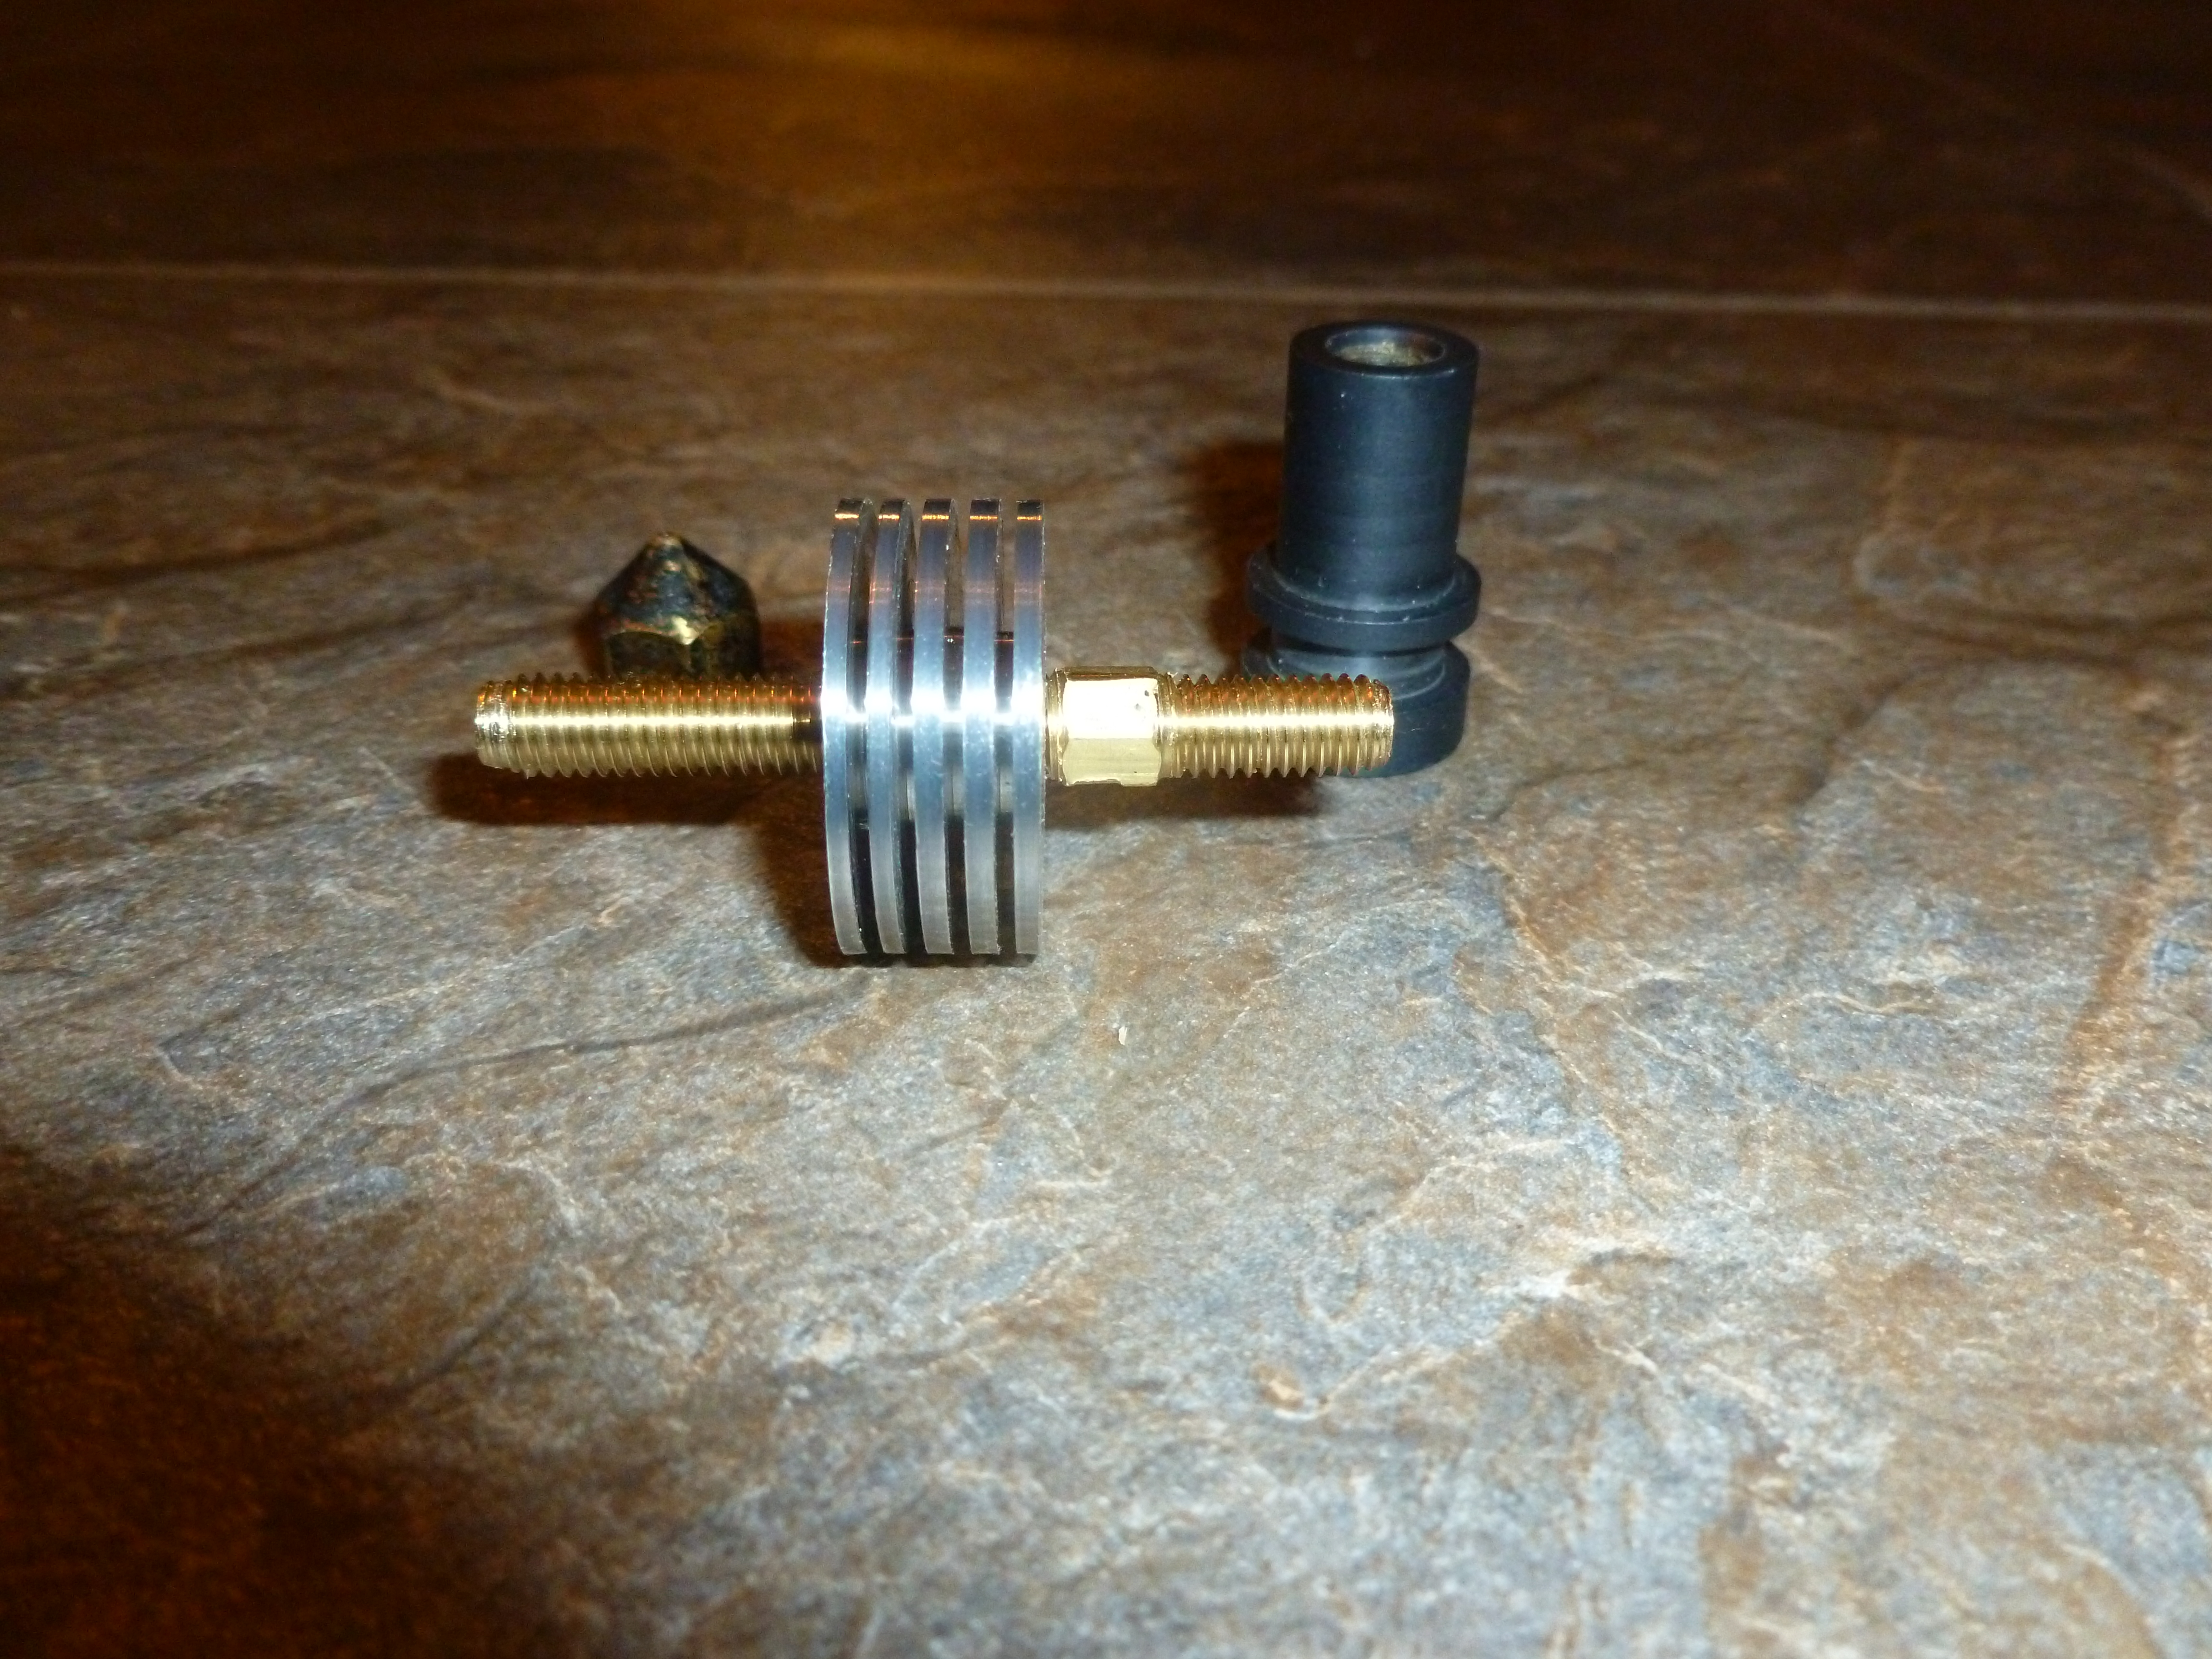
This is my new extruder hot end. After enclosing my printer with an insulated box, I decided that I needed to drop more heat before the plastic entry side of the end of the barrel. I accomplished this by turning an extra long barrel out of brass, and a small heatsink out of aluminum to go between the heater and the Groove Mount.

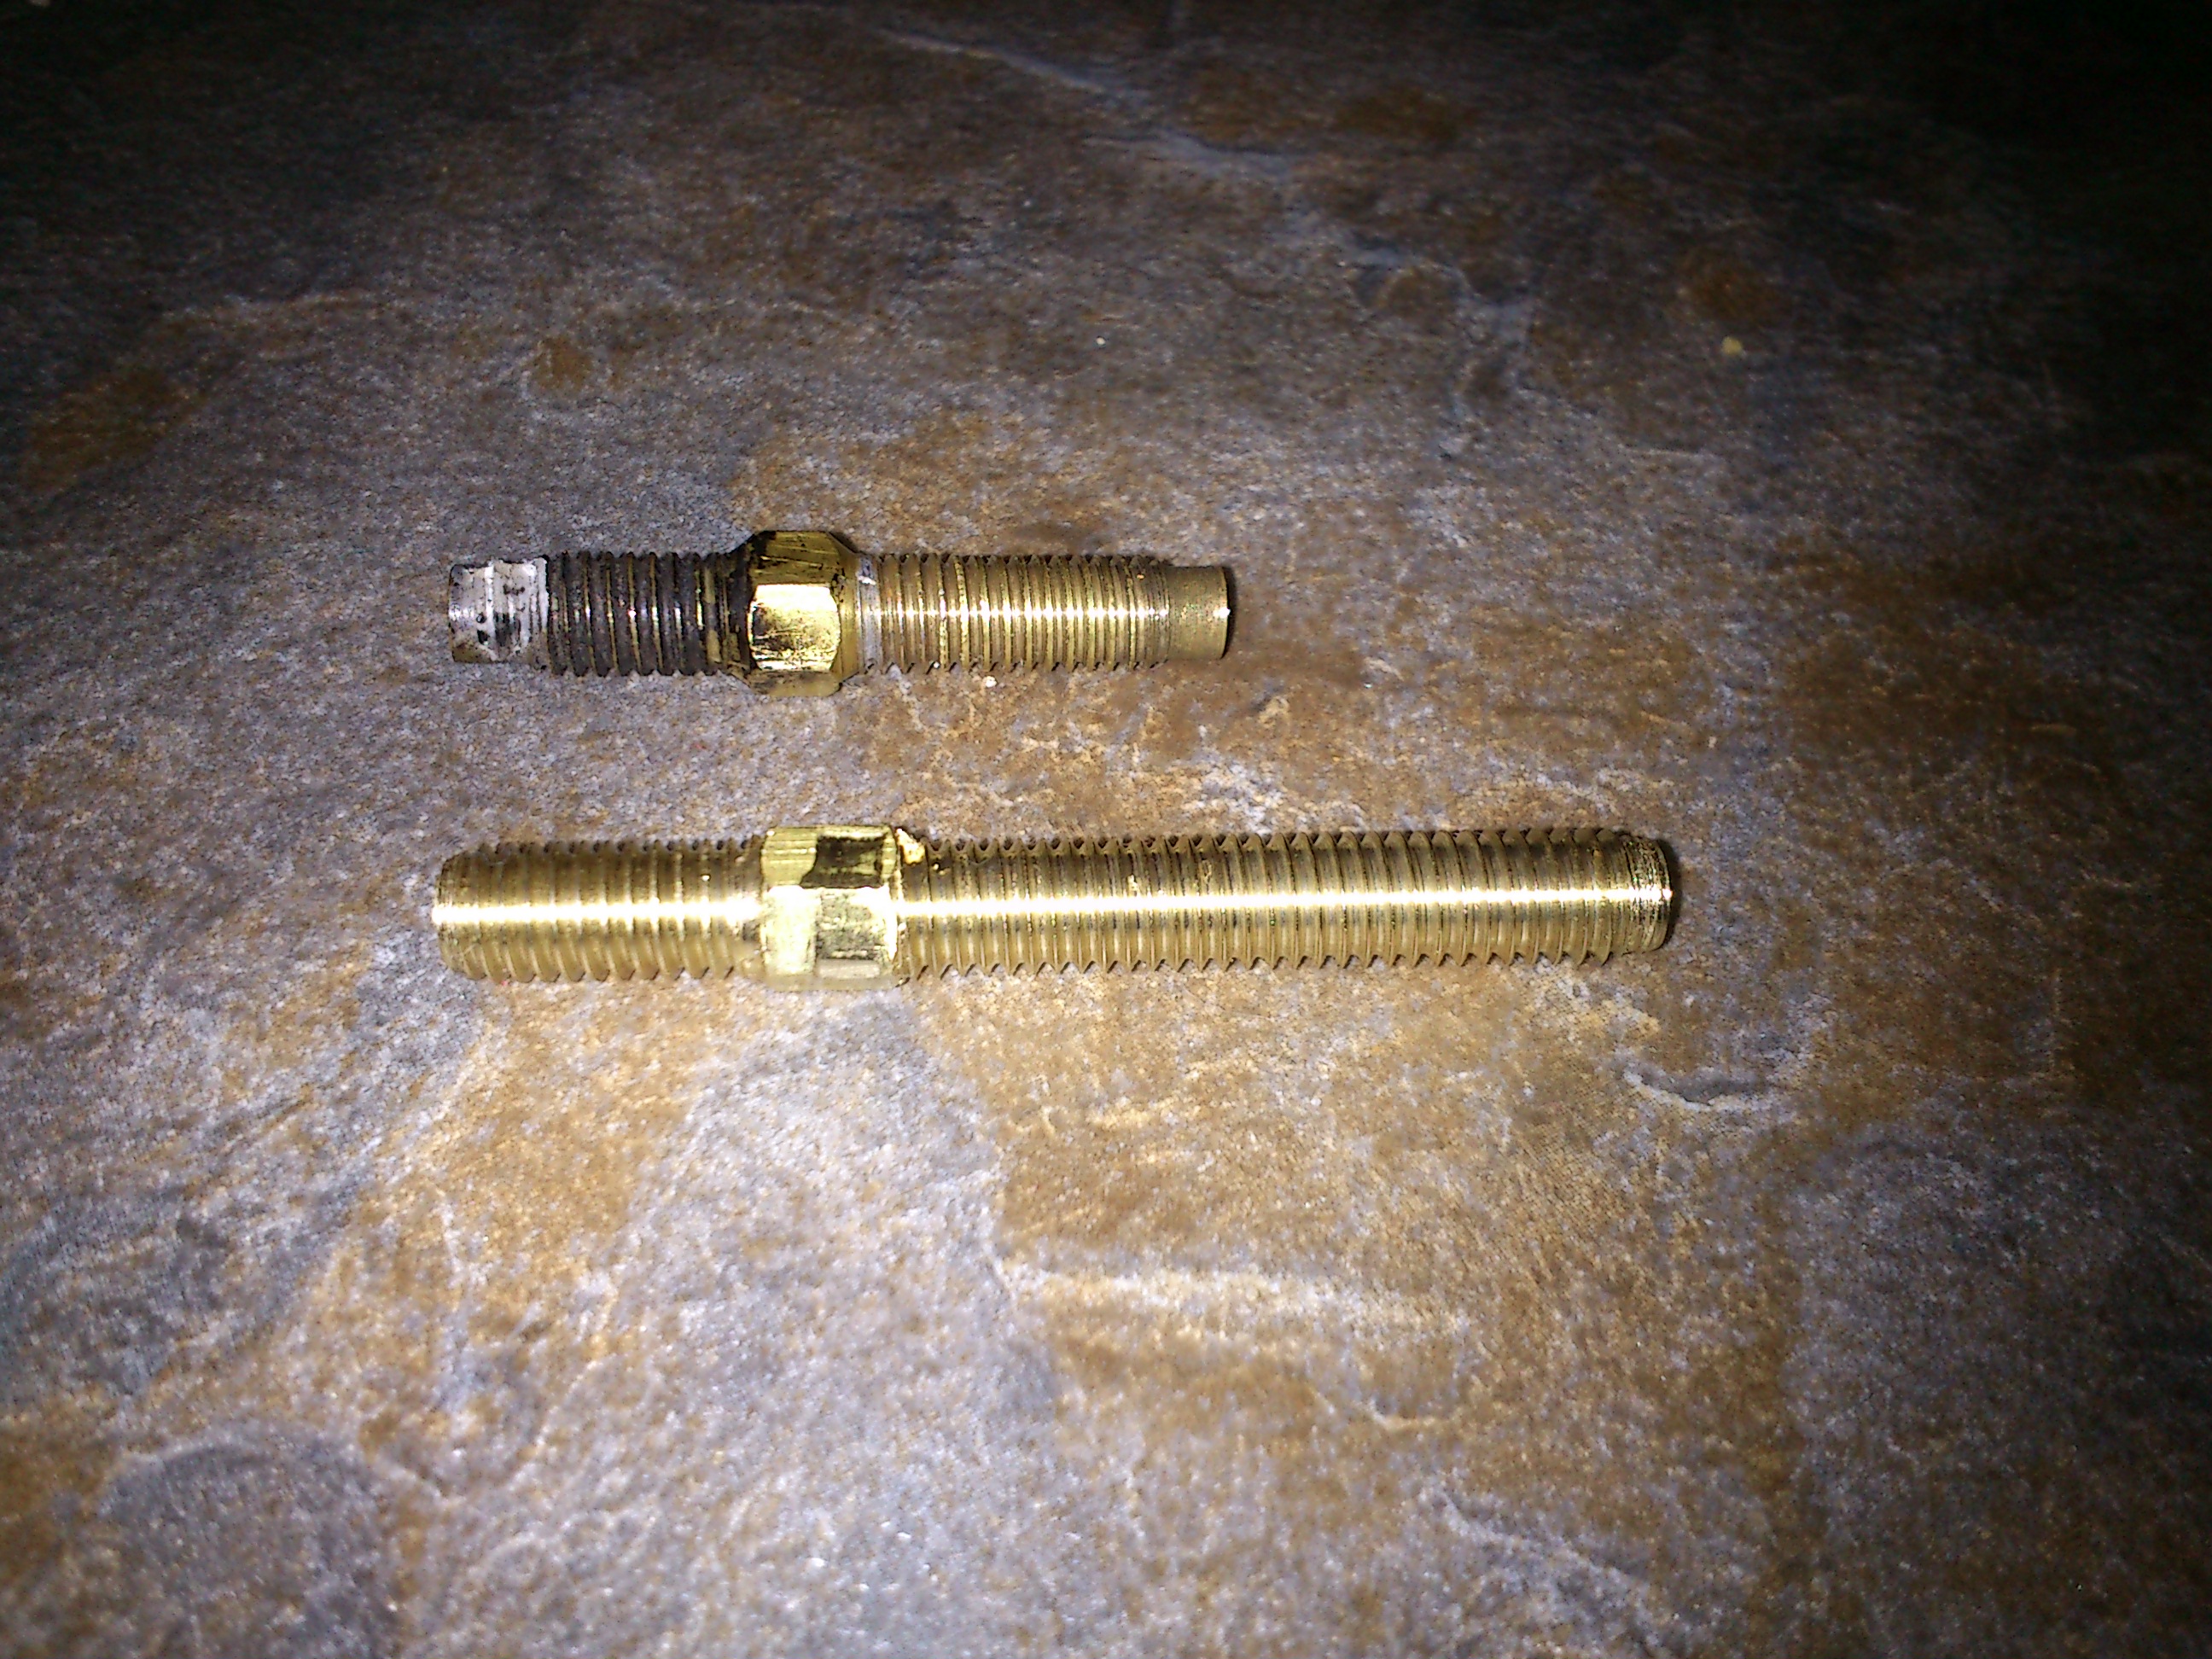
You can see the barrel compared to the original part here:
original_and_replacement_part

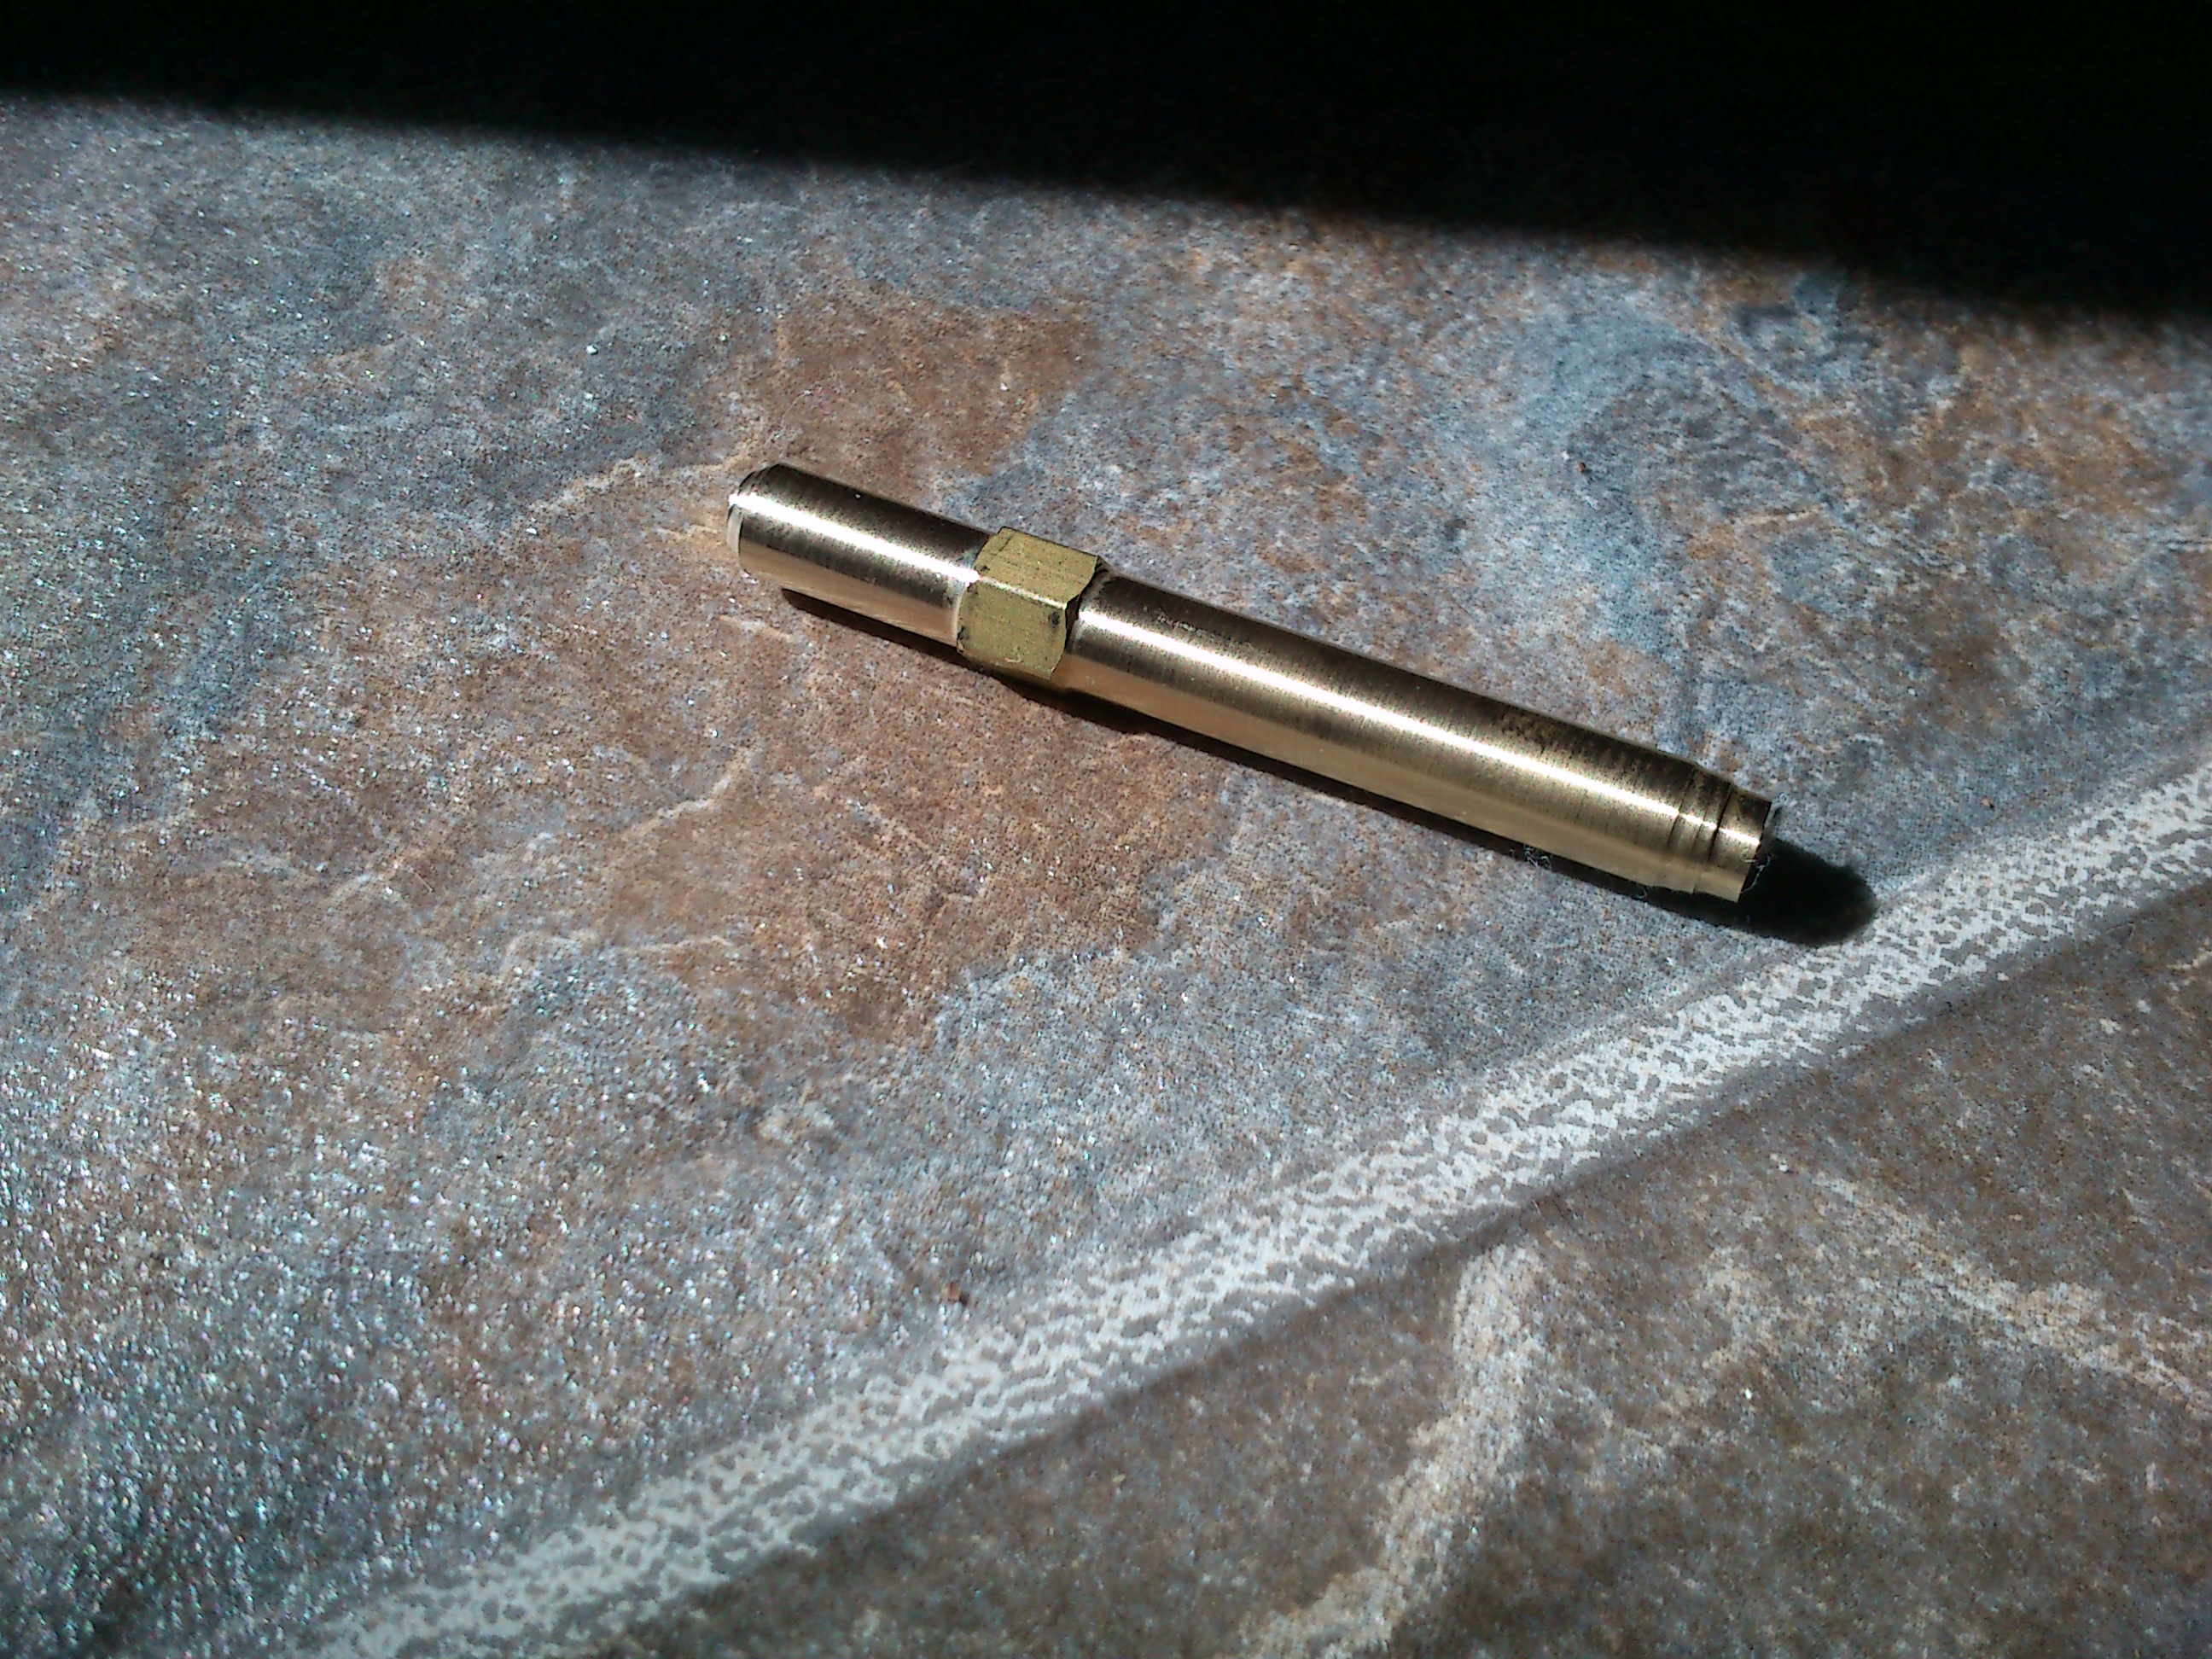
The barrel was straightforward to turn out of a piece of 1/4″ hex stock. I put the threads on with a metric M6x1 die.
turned_hex

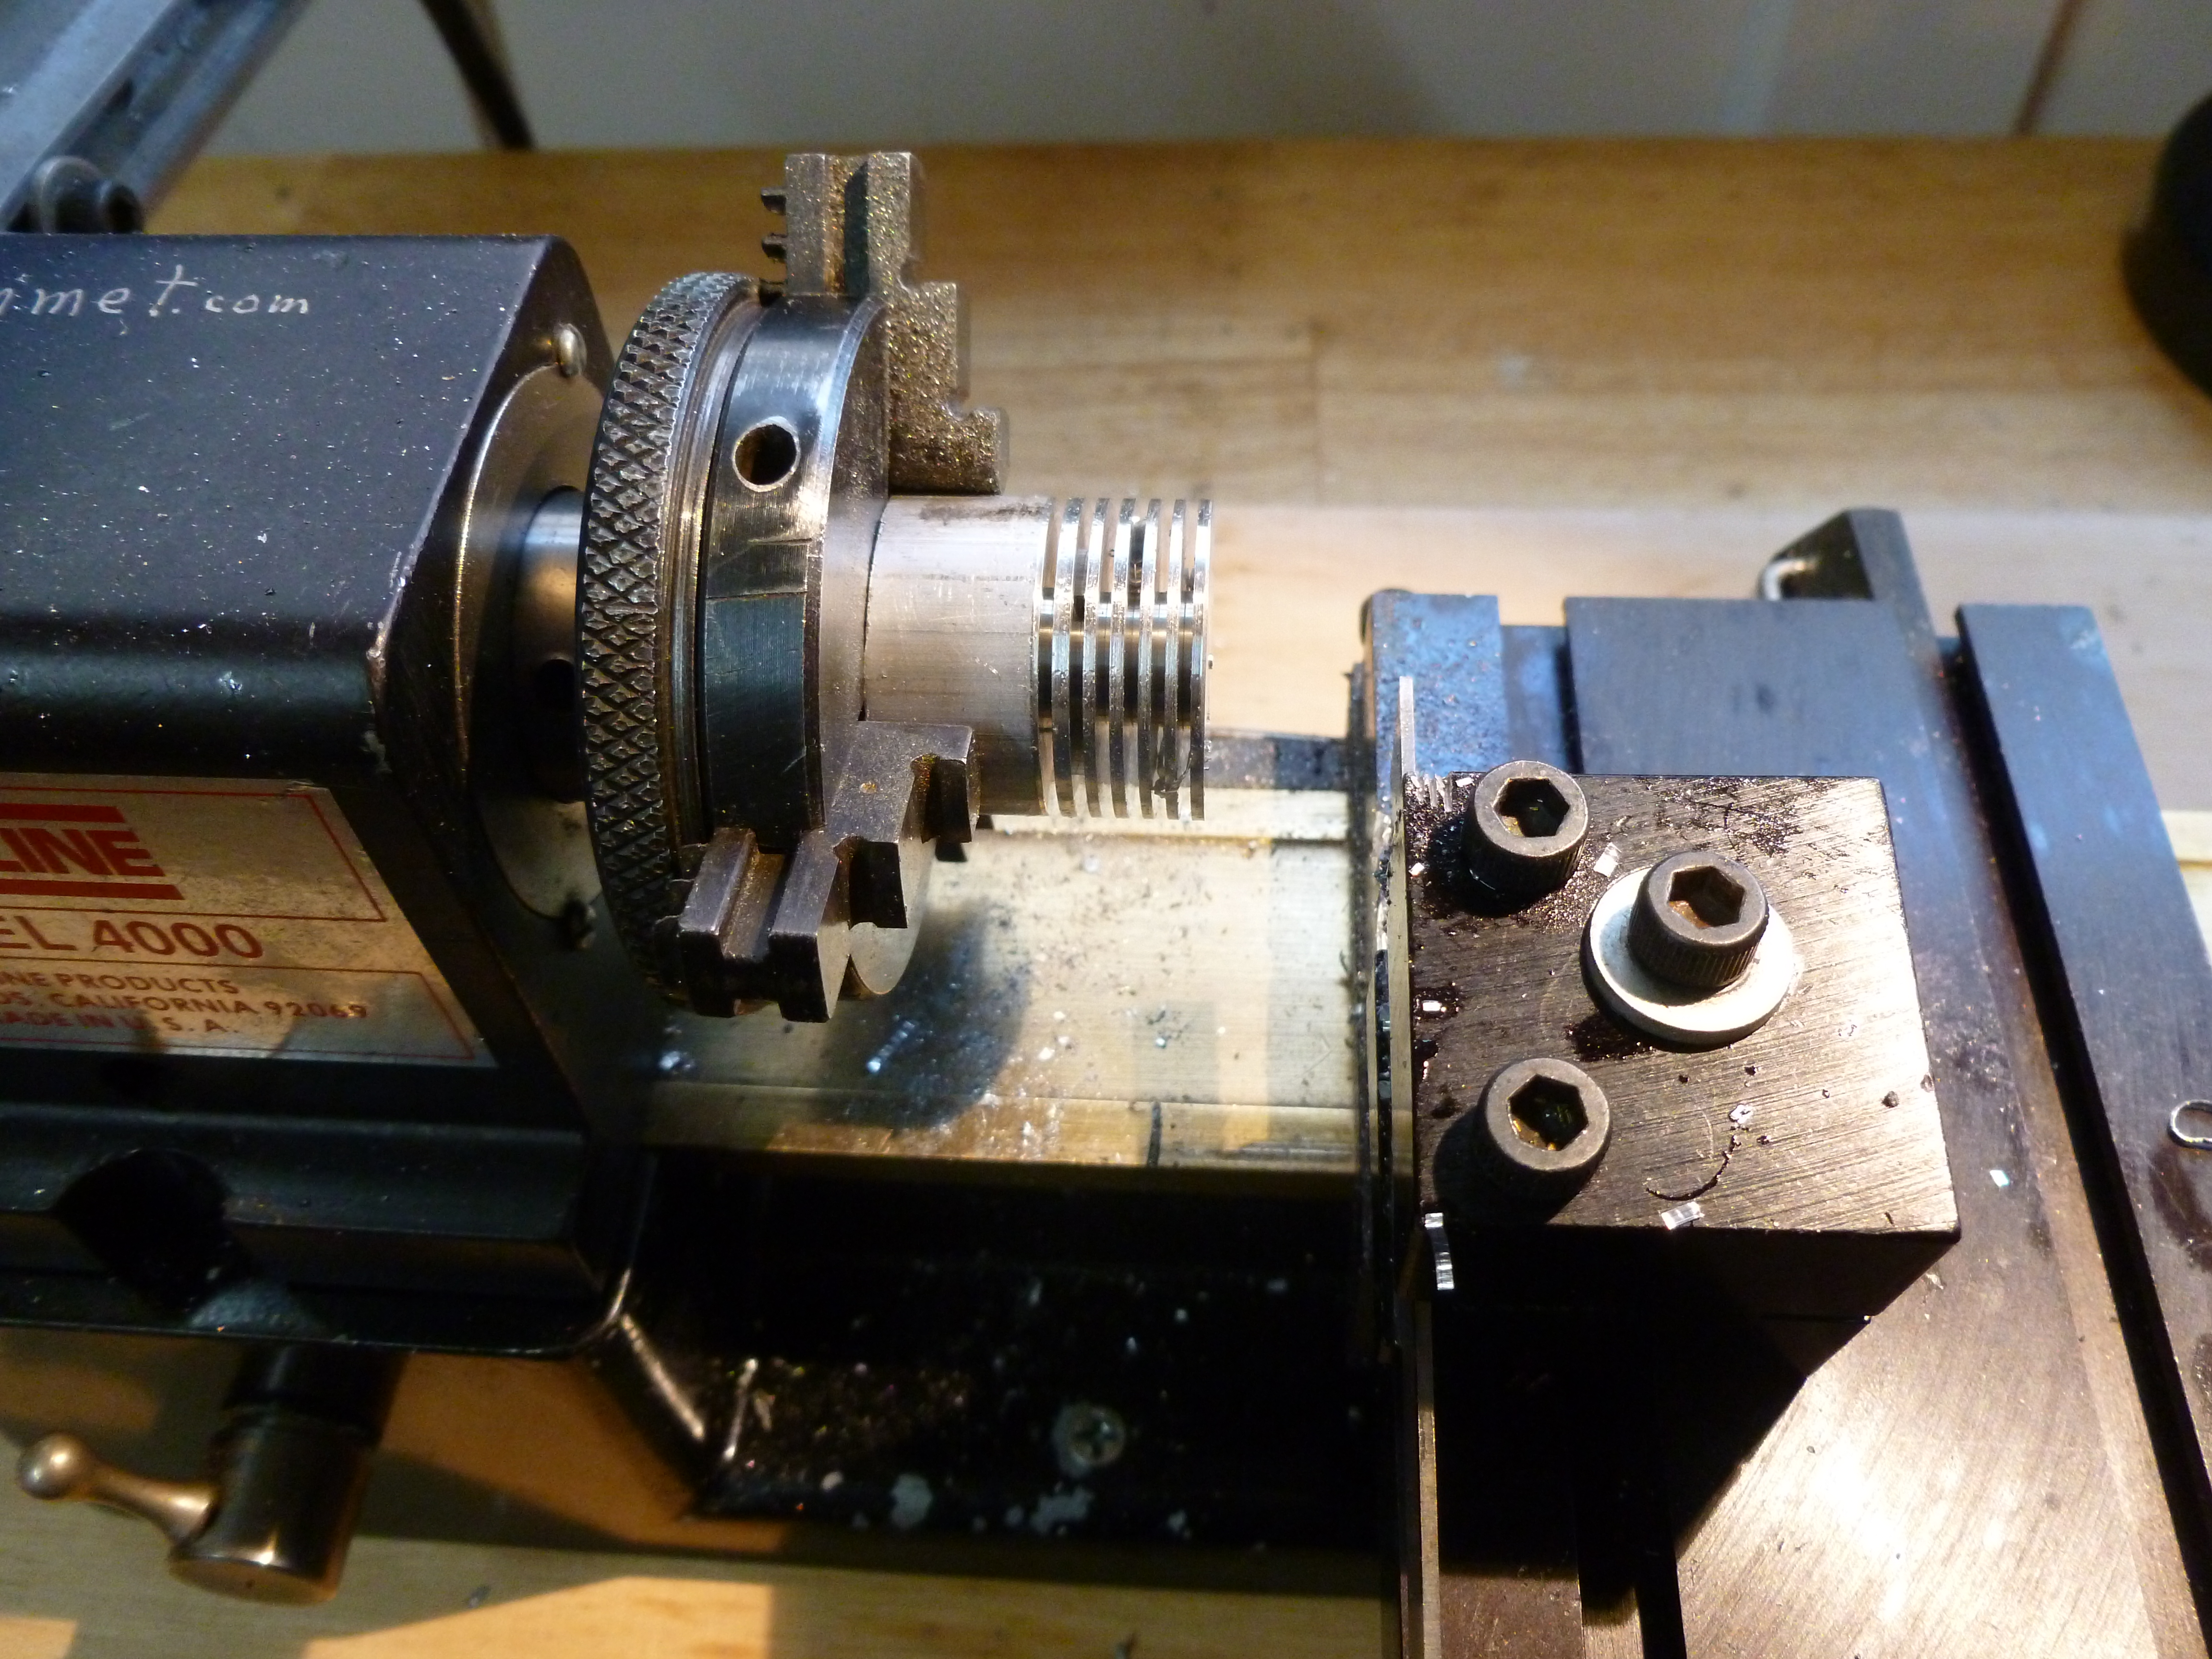
The HeatSink took more time, mostly because I had to cut the fins out of a 1″ diameter rod quite deeply with a cut-off tool.
inLathe1

I compressed the several hours of work on the heatsink down into a six minute video below: